Recyclable Pallets for Sustainable Supply Chains and Reduced TCO
Eliminate disposal costs and turn packaging waste into a recoverable asset for your North Indian operations.
Engineered for the Circular Economy: Your Partner in Green Logistics
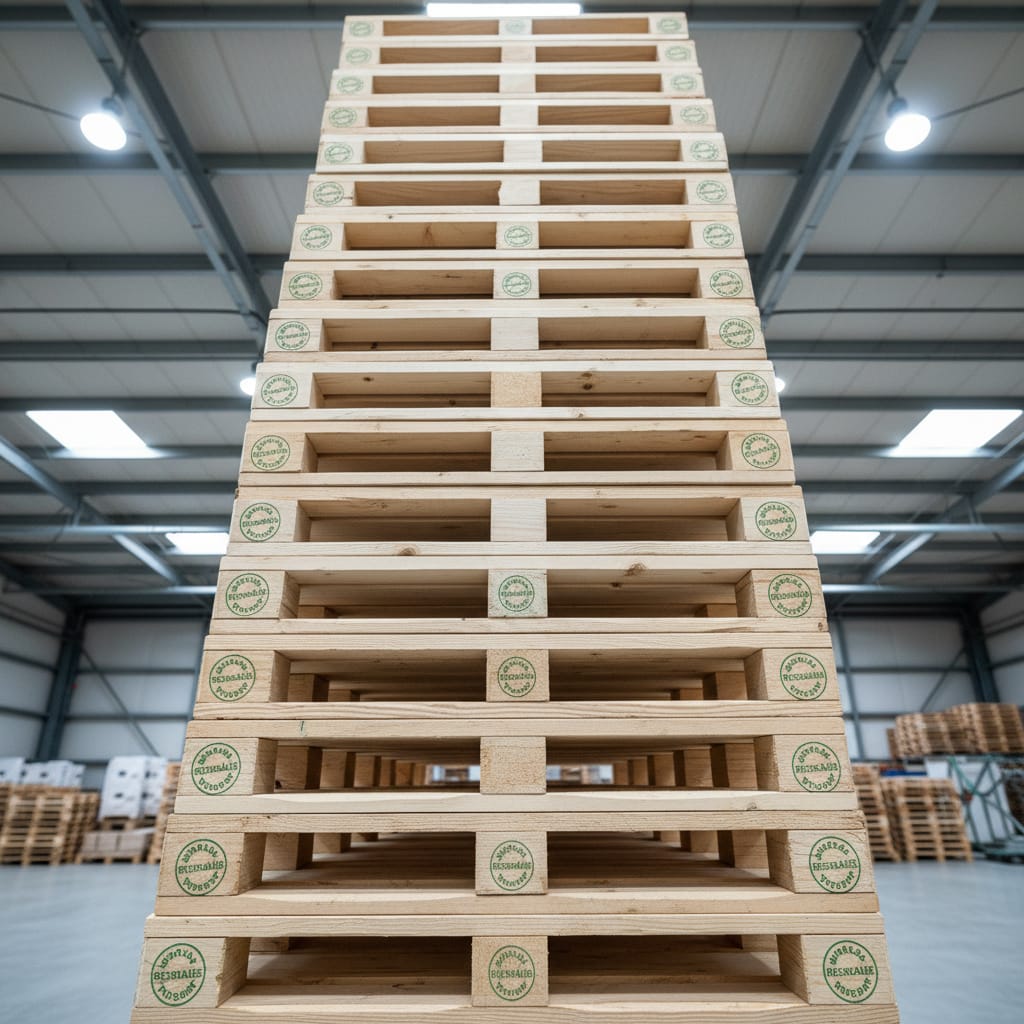
We transition your supply chain from single-use liabilities to recoverable assets through material science. While standard wooden pallets serve a purpose, our recyclable solutions lower your carbon footprint and Total Cost of Ownership (TCO).
Material Science
We manufacture crates, boxes, and pallets from quality timbers such as Spruce and Southern Yellow Pine, delivering lightweight shipping solutions that provide strength, durability, and excellent end-of-life recyclability.
Global Compliance
Our wooden pallets are manufactured to meet strict hygiene handling requirements and are fully ISPM-15 heat-treated and certified, ensuring smooth international shipping while preventing customs quarantine delays.
Supply Chain Speed
Durable construction facilitates optimizing warehouse storage efficiency through repeated use cycles. We ensure your closed-loop system operates without interruption across local hubs like Baddi and Manesar.
Experienced
13+ Years Of Experience
Affordable
Prices
Rustproofed
Corrosion Protection
Punctuality
Delivery Planning and Support
The Technical Edge
Our facility molds units that outperform traditional options in longevity and hygiene. We engineer specific solutions that serve as robust ISPM-15 heat-treated wood alternatives for strict export markets. Whether you require standard dimensions or large-format oversized crates, our production line delivers consistent tare weights. This precision is critical for calculating freight costs in international export shipping.
What We Offer
INDUSTRIAL WOODEN PACKAGING YOU CAN RELY ON
We specialize in manufacturing wooden crates, pallets, and boxes tailored to your specific load requirements.
Genuine people. The Wooden Boxes were strong and neat. Our shipment went a long distance without any damage. The owner is very polite and helpful.
Manish Aggarwal
General Supply
Very fast service. I called them for an urgent requirement and got the material the next day. The Pallet Crate is strong and well built.
H.S. Grewal
Transportation Equipment
Bought standard GMA Pallets from them. Strong wood quality. We use them roughly at the site and they are still in good condition. Highly recommended.
Dinesh S.
Building Materials
Clean finishing on the Wooden Crates. There were no rough nails or sharp edges coming out, so our product remained safe from scratches. Good service by the team.
Rahul V.
Appliance
These Pallet Boxes are very sturdy. We used them for heavy storage and they held up well even after rough use. Delivery was fast which helped us a lot during the busy season.
Gurdeep C.
Agricultural
Good quality Block Pallets. We stack them high in the warehouse and they are very stable. Pricing is also better than the market rates. Reliable supplier for bulk orders.
Praveen L.
Warehouse & Storage
Get a Quote & ROI Calculation
Validated Performance: What is the ROI of Switching to Recyclable Pallets?
Invest in packaging that pays you back through longevity and scrap recovery. Our inventory includes nesting and stackable units designed to reduce return-freight volume. We also offer space-saving collapsible designs for maximum logistical flexibility. Choose these cleaner, chemical-free fumigated alternatives to future-proof your supply chain today.
What is the financial benefit of recyclable pallets?
Recyclable pallets support sustainability by transitioning your supply chain from a linear “use and throw” model to a circular economy. By using pallets made from quality timbers that are 100% recyclable, you eliminate landfill waste and disposal costs. At the end of their lifecycle, these units can be recovered for their scrap value or recycled into new wood products. This lowers your carbon footprint and improves your green supply chain metrics, which is increasingly important for corporate responsibility. Partner with us to reduce waste and optimize your environmental impact.
What is the financial benefit of recyclable pallets?
The financial benefit lies in the Total Cost of Ownership (TCO). While the initial purchase price is one factor, recyclable pallets offer value recovery at the end of their life through guaranteed buy-back options or scrap sales. This contrasts with single-use materials that incur disposal fees. Additionally, their durability allows for multiple use cycles before recycling is necessary, amortizing the cost over many trips. We help you calculate the ROI to show how sustainable choices protect your bottom line. Stop bleeding revenue on waste; invest in recoverable assets.
Are recyclable pallets as durable as standard ones?
Yes, our recyclable pallets are engineered for industrial durability. We use high-quality timbers like Spruce and Southern Yellow Pine to manufacture units that outperform traditional disposable options in longevity. They are designed to withstand the rigors of warehouse storage and transport loops. The “recyclable” tag refers to their end-of-life processing, not a lack of strength during use. You get the same, if not better, load capacity and structural integrity while supporting a greener planet. Validated performance backed by 13+ Years of material engineering experience.
Do you offer ISPM-15 compliant recyclable pallets?
Yes, our recyclable wooden pallets are fully ISPM-15 heat-treated and certified. This makes them suitable for international shipping while still being eco-friendly. You do not have to choose between sustainability and compliance. These pallets meet strict hygiene handling requirements and ensure smooth customs clearance globally. We provide a robust alternative to plastic or composite materials that might be harder to recycle or repair. Choose a solution that is compliant, durable, and sustainable.
Can these pallets be used in automated warehouses?
Absolutely. We manufacture these pallets with precise dimensions to ensure consistent tare weights and compatibility with automated systems. Whether you require standard sizes or large-format crates, our production line delivers the consistency needed for ASRS (Automated Storage and Retrieval Systems). This precision prevents jamming and ensures smooth operation in modern logistics hubs. We combine the benefits of recyclability with the technical specifications required for high-efficiency warehousing. Optimize your facility with our engineered green solutions.

